Resources
 Part of the Oxford Instruments Group
Expand
Collapse
Part of the Oxford Instruments Group
Published: 30 May 2019 · Last updated: 11 Aug 2026
New GaN power electronics are being developed for power conversion and delivery. In electric transportation such as Electric and Hybrid Electric Vehicles (EV and HEV), these devices are becoming increasingly important and device cost and efficiencies are critical for their success. The high mobility and breakdown voltage of GaN make it an ideal material for power devices. In particular, the 2D electron gas occurring at the AlGaN/GaN interfaces allows for very effective devices. However, the AlGaN layer requires a negative voltage on the gate to turn off. Such "D-mode" or "normally-on" devices do not meet fail-safe design criteria and therefore there is a strong drive to develop "E-mode" or "normally-off" devices. There are several strategies to create such devices and using recess etching of the AlGaN barrier is a prominent one. Furthermore, gate dielectric layers are desired to limit leakage currents.
A cross-sectional schematic of an E-mode GaN-on-silicon power device is shown in Fig. 1. Note that various designs have various depths of recess etches, ranging from almost no recess to complete removal of the AlGaN barrier layers and even partly the GaN channel. In all of these cases, a high-quality dielectric and high-quality interface with the dielectric are desired to allow for an E-mode device with low leakage and low power losses. In contrast to other semiconductors, the GaN surface is one of the most process-sensitive in the electronic industry. Therefore, precise control of the applied processes is needed. Several challenges exist around recess etching and gate dielectric deposition which will be discussed further. For the recess etch, the AlGaN layer needs to be etched down to the underlying GaN. This AlGaN layer is thin, typically 20–30 nm and there is no inherent selectivity to GaN for a classic etch process. Therefore, an extremely uniform, reproducible, and slow etch rate is essential to have a satisfactory etch result across a complete 200 mm wafer. For the dielectric deposition, a thin conformal dielectric must be deposited in the recess structure. For both the etch and the deposition the processes should have low damage and result in high-quality interfaces with low defect levels. Plasma processes are desirable here to allow for directional etching and to help deposit high-quality layers at modest thermal budget. The reactive species in the plasma such as radicals and ions mean that etching is facile and high-quality material can be deposited as well. However, it also means that the energy and fluxes of the species must be carefully managed to limit damage to the device.
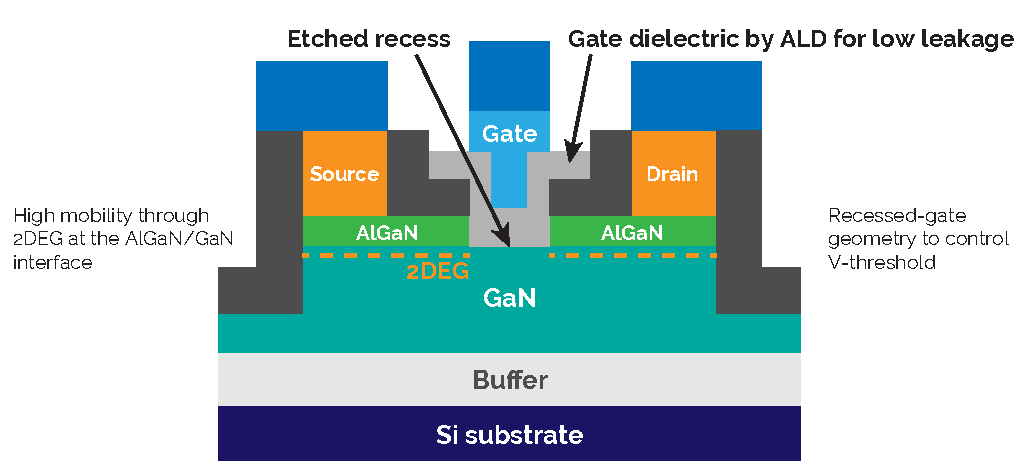
Fig. 1 — E-mode GaN-on-silicon power device. Using a recess etch and a gate dielectric can allow for a normally-off device with low leakage and low power losses. Atomic Scale processing techniques such as ALD and ALE are needed to control etch and deposition and have low damage to the sensitive interfaces.
Atomic Scale Processing (ASP) techniques such as Atomic Layer Deposition (ALD) and Atomic Layer Etching (ALE) can provide the control and low damage processing needed for these devices. In addition, in-situ surface pre-treatments before ALD or ALE can clean and modify material interfaces to reduce defects and improve device performance. Highly conformal ALD films can follow the 3D recessed-gate geometry. Furthermore, ALD films with excellent electrical properties provide effective passivation and isolation of the device. The sensitive surface of GaN can benefit greatly from a combination of ASP techniques to minimize interface states and border traps. To avoid exposure to air between processes, Oxford Instruments' tools can be clustered together such as illustrated in Fig. 2.
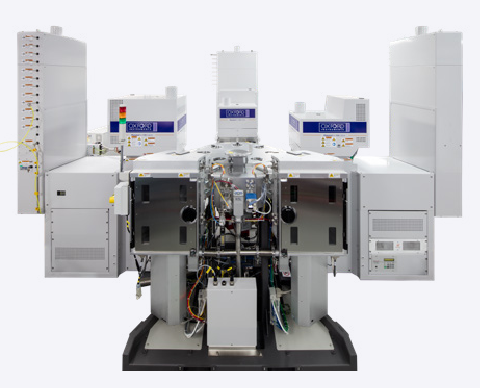
Fig. 2 — For easy, inert handling between process modules, our systems can be clustered together with ALD and ALE modules. A robotic handler transfers wafers between the chambers for processing. Cassette to cassette handling solutions are available for high volume manufacturing.
In this whitepaper, we explain the basics of ALD and ALE, relevant for GaN power devices and low damage plasma processing. We will then describe and discuss device examples and strategies for GaN power devices, including pre-treatments and atomic scale processing.
In ALD, thin films are grown in cycles where the surface is exposed to various gas-phase species in alternating doses, isolated by evacuation or inert purging. Essential to ALD is that the reactions are self-limiting, which means for instance that only a single layer of precursor can adsorb on the surface or that removal of surface groups does not result also in removal of the surface below if exposures are too long. A sub-monolayer of material is deposited in each cycle which consists of four basic steps: (i) A precursor dose where a precursor is typically an inorganic metal-organic or metal-halide (e.g. Al(CH3)3); (ii) an inert purge and/or pump step; (iii) a co-reactant step, typically involving a small molecule (e.g. H2O or O2 plasma); and (iv) a purge and/or pump step. For the precursor, the element to be deposited is in many cases the metal center (e.g. Al), while for the co-reactant, it is typically a non-metal such as O. ALD cycles are repeated to deposit a desired thickness of film (e.g. Al2O3). ALD can provide the following benefits: precise thickness control by tuning the number of cycles; conformal coating even in high aspect ratio structures due to the self-limiting nature of the precursors; low pin hole levels; very thin and dense films; wide variety of materials possible, especially with plasma-enabling; and deposition temperature range down to room temperature. Fig. 3 illustrates the metrics that are important for covering a substrate with 3D features. Coverage of the planar surface is evaluated using the uniformity while the coverage of 3D features is evaluated using the conformality. The growth control over the film thickness itself is another important metric. The ability to achieve these metrics at low temperatures is an additional important aspect.
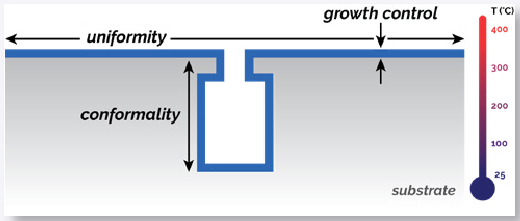
Fig. 3 — The coverage metrics of a film on a substrate with 3D features.
Water vapour is the most reported oxygen source for metal oxide ALD. However, due to the high sticking coefficient of water, it adsorbs strongly to surfaces and is difficult to purge from the reactor, especially at low deposition temperatures (e.g. ≤100 °C). Water is also often insufficiently reactive at low temperatures to result in high-quality films. Similarly, NH3 can be used for the growth of nitrides, but can be difficult to purge and insufficiently reactive. Plasmas can be used as co-reagents to increase reactivity and grow films that would not otherwise be possible via a thermal ALD route. The plasma species are generated close to or inside the ALD reaction chamber. When employing a plasma, various highly reactive species can contribute to the surface chemistry, such as radicals and ions (e.g. O and O2+). In the case of a remote plasma (as in Oxford Instruments Plasma Technology ALD systems), both radicals and ions can be present, and their levels can be tuned to optimum levels by changing the plasma power and pressure.
ALE is a relatively new method that can be used to etch with great accuracy. In this atomic scale process, fast-switching is used to alternate between a step that creates a modified surface layer and an etching step that removes only this modified layer, leaving the underlying atoms undisturbed. Similar to ALD, these steps are separated by inert purging and precursors are self-limiting in nature. The technique enables very high etch control. Low etch rates down to 1.8 nm/min can be repeatedly achieved which furthermore can have the benefit of low substrate damage. The ALE processes considered for power electronics are anisotropic and plasma-based (there also exist thermal and isotropic ALE processes). The most common example of an ALE process uses Cl2 plasma and Ar+ ions. Here, Cl radicals chlorinate the surface of the material to be etched and Ar+ ions remove this chlorinated layer. The self-limiting nature is present since after chlorination of the top surface the subsurface is slow to chlorinate and the ion energy chosen for Ar is sufficient for removal of the top chlorinated layer, but below the sputter threshold for the bulk material. Note that plasma can be on throughout cycle (or be switched on/off) as long as the ion energy in the purge steps is low enough to negligibly remove the chlorinated layer.
Fig. 4 shows the Etch Per Cycle (EPC) as a function of the bias voltage during the Ar plasma step for AlGaN ALE using Cl2 plasma and an Ar plasma. The sputter threshold can be explored when investigating the process with no Cl2 in the cycle. It can be seen that around ~18 V of DC bias there is sufficient ion energy to remove the chlorinated layer but insufficient energy to sputter. An ALE tool is a specialized RIE-ICP module with fast-acting valves and fast-switching control that enables the rapid alternating between the four steps of i) dose; ii) purge; iii) etch and iv) pump steps. Furthermore, the biasing hardware is such that extremely low bias power can be applied reproducibly.
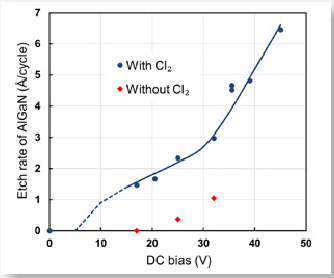
Fig. 4 — The etch per cycle (EPC) as a function of the bias voltage during the Ar plasma step for AlGaN ALE using Cl2 plasma and an Ar plasma. The sputter threshold can be explored when investigating the process with no Cl2 in the cycle. It can be seen that around ~18 V DC bias there is sufficient ion energy to remove the chlorinated layer but sputtering is negligible.In standard plasma etching, the roughness would normally increase (slightly) with increase in etch time. However, in ALE, the etch can actually smoothen a somewhat rough AlGaN surface, as shown in Fig. 5. The insets indicate AlGaN surface roughness before etching and after 200 ALE cycles. Note that other ALE chemistries have been explored for GaN and AlGaN such as using N2O plasma and BCl3 plasma with bias. The N2O allows for controlled oxidation of the surface and the BCl3 etch step removes this oxidised layer. Depending on the device requirements a certain chemistry might be preferred.
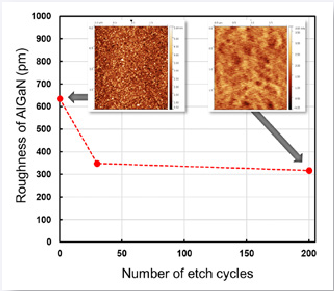
Fig. 5 — Effect of ALE on roughness of AlGaN surface. A reduction in roughness with the number of ALE cycles is observed. AFM data courtesy of Paolo Abrami in collaboration with Bristol University.
Many thermal processes are inherently low damage, but often do not provide the reactivity required to achieve a well-functioning device. The plasma processes discussed in this paper can, in principle, be done in a wide range of plasma systems but to be suitable for GaN devices the plasma conditions should be low damage which can be a challenge for many system configurations. Damage by the plasma has been a long-standing topic of interest for plasma ALD but few in-depth studies have been performed and insights are relatively recent. Here, "damage" is defined as creation of electronic defects or as undesirable changes to composition or structure of materials caused by exposure to plasma species. Using a remote plasma such as ICP is a method to reduce the density and energy of ions and photons near the surface which might cause such damage. Three main categories of plasma reactors have been distinguished: direct plasma, remote plasma, and radical enhanced as shown in Fig. 6. In the case of direct plasma, the substrate on which deposition is carried out is positioned within the main plasma zone and is involved in plasma generation. For a remote plasma, the substrate on which deposition is carried out is positioned outside of the main plasma generation zone. Control of parameters can make the plasma "more" or "less" remote by reducing or enhancing the flux of species toward the wafer, respectively. The term "radical-enhanced" is generally used to describe configurations where only the radicals can reach the substrate area.
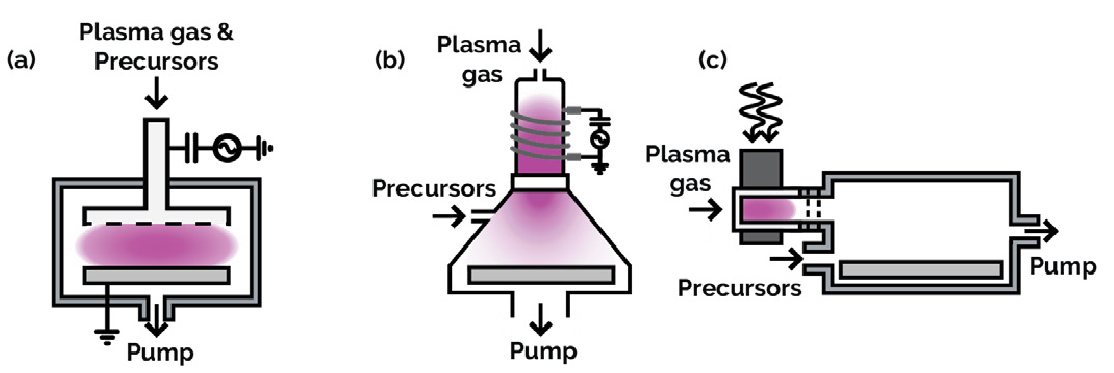
Fig. 6 — Three main classes have been distinguished, labelled as a) direct plasma, b) remote plasma, and c) radical enhanced.
Control of plasma species is needed to have the optimal benefit from the plasma species to get high film and interface quality but at the same time negligible damage. Some ion energy can improve film quality and properties, particularly for nitrides and at lower deposition temperatures. Certain interfaces and substrates can be sensitive to ion energy leading to possible device damage. Ion energies can be carefully controlled in Oxford Instruments Plasma Technology (OIPT) systems using our own designed and manufactured plasma sources, which allow maximum benefit of plasma whilst minimising damage to the substrate. In both ALD and ALE plasmas users want to control or limit the ion energy but in ALE a relatively high ion flux is needed, while in many ALD conditions ion flux must be reduced as well. Our OIPT plasma systems allow this detailed level of plasma tuning and enable the best possible process conditions.
While plasma ions and photons are important, the chemical effects of plasma species and radicals must not be overlooked. O2 plasma radicals can oxidize the GaN surface which can adversely affect the threshold voltage. Radicals from H2, N2, and NH3 plasmas can be used to reduce surface damage and can remove oxygen and carbon while adding nitrogen to the surface. Generally, varying pressure and plasma power in ICP systems allows the minimization of the ion energy and flux. Note that ion energies of ~20 eV were found to not negatively affect device performance. For instance, the H2 plasma pre-treatments performed by Kerr et al. led to low defect densities while the plasma power of 100 W and plasma pressure of 20 mTorr indicate such ion energies.
Defect levels should also be compared after complete processing and all temperature steps involved. For example, in Si passivation using ALD Al2O3, before anneal steps the thermal process has better passivation, while after anneal plasma ALD Al2O3 was found to have the best passivation properties. Such knowledge from other fields could be useful for power semiconductors as well.
In general, III-V surfaces such as GaN can have a wide range of surface impurities or defects (for instance carbon contamination, native oxides, and vacancies). After deposition of the dielectric these can form interface states and border traps depending on the processing used as shown in Fig. 7. The trapped charge can also change with time which can cause a shift in the threshold voltage over time and result in instability of operating characteristics of transistors. Furthermore, fixed and trapped charge can both scatter the carriers in the channel, which can lower the carrier mobility.
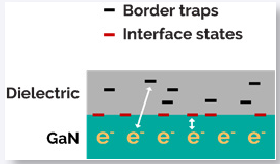
Fig. 7 — Interface states and border traps can be present at and near the interface between GaN and a gate dielectric. Charges can trap and detrap in these states resulting in unwanted device behaviour.
To achieve a low defect density at the interface of GaN and the gate dielectric, a variety of surface treatments and cleans are considered. In general, such a treatment could be a gas phase chemical exposure or a plasma with an optimized plasma pressure, power and gas flow. These can be done to improve nucleation for certain surfaces, improving adhesion and most importantly to do in-situ cleaning. One possibility of doing surface treatments would be doing the treatment in situ, in the ALD tool itself as for example for the data in Fig. 8.
The treatment could be a plasma surface treatment (e.g., H2, N2, Ar, NH3 plasma) or exposure to a gas or chemical vapour. These could be run in pulses and alternated in a similar fashion as an ALD cycle. An interesting effect that can be used is the self-cleaning effect of TMA, which is the typical ALD precursor for Al2O3. TMA is a reducing agent which can for instance reduce some compound semiconductor oxides, while forming Al2O3. Note that besides TMA, a wide range of ALD precursors could be of interest as a pre-treatment to clean-up the native oxide on III-V materials. Kerr et al. demonstrated that doing H2 plasma exposures alternated by TMA exposures as a pre-treatment resulted in low defect density (Dit) values. Son et al. found that in their case they had even lower defect density values when alternating N2 plasma exposure by TMA exposures prior to the dielectric deposition. The clean-up effect by pulses of ALD precursors is expected to consume surface oxide of the III-V and convert the III-V oxide partly into the ALD oxide (e.g., TMA converting GaOx on GaN into Al2O3). Note that the resulting ALD oxide remains and is used, for instance, as a part of the dielectric stack in a device. An example of a pre-treatment before ALD is indicated in Fig. 9 with the example of a plasma pre-treatment before a plasma ALD process. The clean-up by exposure to N2 plasma, H2/N2 plasma, or H2 plasma presumably removes carbon and oxygen from the surface, and nitrogen-based plasmas are specifically suggested to fill in nitrogen vacancies or cause nitridation of the surface. These effects can be a "clean-up" effect to revert a partly oxidized GaN surface to a pristine state.
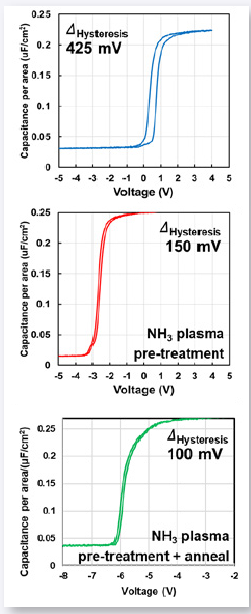
Fig. 8 — A low power, low damage NH3 plasma pre-treatment was used to determine the impact on GaN HEMT performance. The capacitance-voltage (CV) hysteresis is reduced from 425 mV to 150 mV with the optimised NH3 plasma pre-treatment indicating a reduction in the interface traps at the GaN/Al2O3 interface. The CV hysteresis is reduced further to 100 mV by performing a high temperature anneal in forming gas which is a standard process for GaN HEMTs.
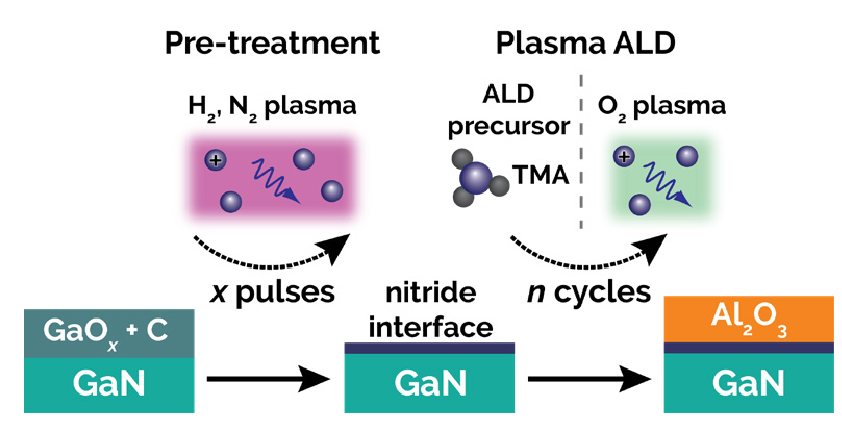
Fig. 9 — Example of pre-treatments and ALD on GaN to first clean-up the GaN surfaces and then deposit the ALD dielectric. The example of H2 or N2 plasma pre-treatment and Al2O3 plasma ALD is illustrated. The plasma pre-treatment not only can remove carbon and oxygen from the surface but can furthermore cause nitridation of the GaN-dielectric interface.Ar plasma has also been reported as a useful pre-treatment. These improvements in performance in both the MOS capacitors and the MISHEMT devices might be attributed to either the removal of native GaOx before the deposition of the gate oxide, reducing the number of interfaces near the GaN surface or from the formation of higher quality GaOx with fewer electronic traps.
Furthermore F-implantation is also considered as a treatment to achieve E-mode devices. This has for instance been demonstrated using an ICP etching chamber before 20 nm thermal ALD Al2O3 gate insulating dielectric layer. Note that our ALD systems can also run fluorine plasmas so this treatment could also be performed in the ALD chamber beforehand if desired.
For InAlN/AlN/GaN HEMTs both thermal and plasma ALD Al2O3 demonstrated a very low gate leakage current, while a lower dispersion was observed for plasma ALD Al2O3 compared to thermal ALD. Note that although surface treatments are often mentioned, there are also cases where without such treatments good results are obtained. For instance Kanamura et al. report E-mode GaN MIS-HEMTs with a high drain current using plasma ALD Al2O3. Possibly the remote O2 plasma in the ALD process combined with the anneal used afterwards result in a high-quality interface.
Another approach is the growing of ALD nitride interface layers followed by an oxide dielectric (either by plasma or thermal ALD). Liu et al. demonstrated epitaxial growth of 4 nm AlN on GaN on which they deposited 10 nm ALD Al2O3 resulting in a dielectric stack with excellent device performance for thin film transistor devices. Such a strategy might also be of interest for GaN HEMT devices. Similarly, N2 plasma can be used to create a thin nitride interlayer. Putting all processing steps together in the right way will be crucial for the resulting device. Huang et al. for instance showed that with a combination of wet cleaning of the etched surface, in-situ remote-plasma pre-treatments, ALD of the Al2O3 gate dielectric and post-dielectric annealing allowed for high performance E-mode Al2O3/AlGaN/GaN MIS-HEMTs featuring good Vth-uniformity.
Due to the control of the ALD process it is relatively easy to include dopants or make mixed materials. For instance fluorine-doped Al2O3 has been used to control the threshold voltage. In this work F:Al2O3 was deposited by thermal ALD in which the H2O precursor was replaced with a 40% NH4F:H2O solution. Alternatively you could utilize SF6 plasma treatments to deposit AlF3, to dope Al2O3 by fluorine. By alternating ALD processes in a so-called "supercycle" it is also relatively easy to make alloys or mixed oxides. One example from the literature is MgxCa1−xO where the composition was tuned to have low lattice mismatch with the GaN lattice to promote epitaxial growth.
The metal-dielectric interface is of equal importance to that of a semiconductor-dielectric interface since it determines the threshold voltage of completed transistors. Therefore the gate metal has also been considered to be grown by ALD. TiN is a promising gate material. Conductive nitrides such as TiN can benefit from plasma ALD as well as the ability to control or enhance ion energy by substrate biasing. To avoid damage to the interface the first few nm of TiN might need softer plasma conditions which can easily be accomplished by changing plasma pressure and power in a remote plasma which is a recipe setting. Other elements and metal nitrides can be mixed in, in case the work function would need to be tuned (e.g., add in AlN, WNx, HfNx).
Fig. 10 shows the comparison of a D-mode and E-mode GaN HEMT device. The final device fabrication was done at the University of Glasgow. The process used Ar/Cl2 etch chemistry. A clear shift in the Vth from −5 to +0.15 V was observed.
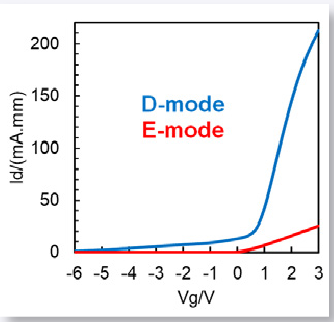
Fig. 10 — I-V curve comparison of a D-mode and E-mode GaN HEMT device. Device fabrication at University of Glasgow. Vth shifts from −5 to +0.15 V when going from D-mode to E-mode by recess etching.Thayne et al. explored ALE using bromine-based chemistry in order to have products that are removed at lower Ar ion energies. In the final optimised process, HBr diluted in Ar in a ratio 7:42 sccm flowed across the sample surface (no plasma was struck). This process enabled etching with an Ar plasma power of 20 W. For this HBr:Ar ALE process, an 0.13 nm/cycle etch rate was obtained with rms surface roughness of 0.9 nm, similar to that before etching. The ability to reduce the Ar plasma power to 20 W had a significant impact on the etch-induced damage, as determined by van der Pauw measurement at room temperature. No modification to the electron mobility and carrier concentration and therefore sheet resistance of single barrier AlGaN/GaN structures as a consequence of 60 second exposure to Ar plasma powers of less than 25 W was observed. The HBr/Ar based ALE process therefore seems to be an encouraging one for controllable etching in the gate region of GaN-based power electronic devices, as etch rates of around 0.13 nm/cycle can be maintained but with minimal Ar plasma etch induced damage.
Atomic Scale processing techniques such as ALD and ALE have the ability to provide the control and low damage processing needed for these devices. In addition surface treatments performed in ALD or ALE reaction chambers can clean and modify interfaces for reduction of defects and improvement of properties. ALD produces conformal films adapted to small recessed gate geometry. ALD can furthermore provide effective passivation and isolation through excellent electrical properties. Surface pre-treatments have been indicated to be essential to enhance device performance. The combination of techniques should be ideal for the sensitive interfaces present and to minimize interface states and border traps as demonstrated by many examples.
© Oxford Instruments 2026